Listening to Steel: The Vibration Analysts Who Predict Machine Failure Before It Happens
The Warning Nobody Heard
The compressor at a chemical processing plant in Louisiana ran for eleven days after the first sign appeared. The sign was not a warning light. It was not an alarm. It was a shift in frequency—a subtle harmonic deviation measurable only in thousandths of an inch of displacement per second. No one was listening closely enough to catch it. When the machine finally failed, it took three days of production offline and cost the facility roughly $2.4 million in lost output, emergency parts, and contract labor.
The plant hired a vibration analysis team six weeks later.
A Field Discipline Built on Physics
Vibration analysis is not a new science, but its application as a real-time field diagnostic discipline has grown substantially over the past two decades. The fundamental premise is straightforward: every rotating machine produces a unique vibration signature, and deviations from that baseline indicate developing faults. What makes the field demanding is the interpretive skill required to distinguish meaningful anomalies from mechanical noise.
Certified vibration analysts—many of whom hold credentials through the Vibration Institute or the International Organization for Standardization's machinery condition monitoring standards—work with accelerometers, proximity probes, and portable data collectors to gather readings from motors, pumps, fans, gearboxes, and turbines. The data itself is only raw material. The expertise lies in reading it.
"You're looking at a spectrum and asking what it's telling you," said one senior analyst with more than two decades of experience in petrochemical facilities across Texas and the Gulf Coast. "A bearing defect frequency at two times running speed means something very different than a resonance peak near the natural frequency of the structure. Context matters enormously."
What the Frequencies Say
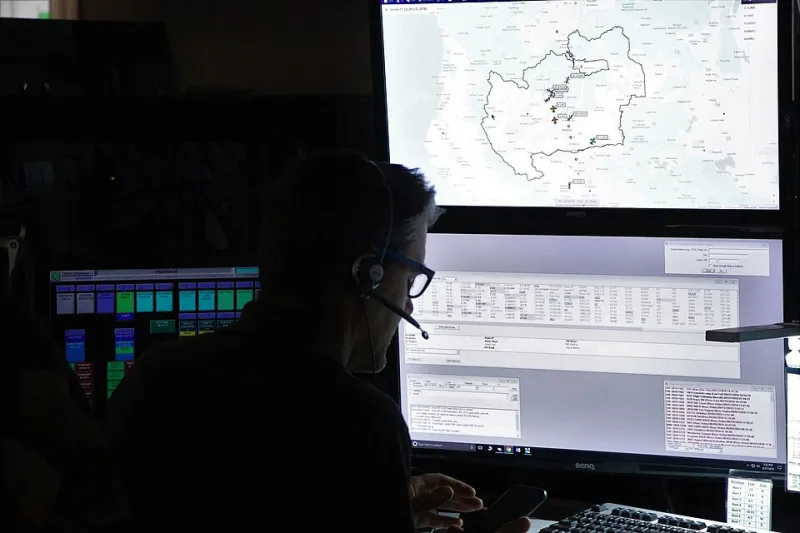
The diagnostic vocabulary of vibration analysis is precise and layered. Analysts examine overall vibration levels, but the real intelligence lives in the frequency domain—specifically in the fast Fourier transform spectrum, which breaks a complex vibration signal into its component frequencies.
Outer race defects on rolling element bearings produce characteristic defect frequencies that can be calculated from bearing geometry. Misalignment between a motor and pump generates dominant peaks at one and two times the running speed. Looseness appears as a forest of harmonics. Cavitation in a pump creates broadband energy in the high-frequency range. Each fault has a fingerprint, and experienced analysts can identify multiple developing problems simultaneously from a single data set.
Acoustic emission testing extends the diagnostic range further. High-frequency stress waves generated by micro-cracking or metal-to-metal contact propagate through machinery structures in ways that standard vibration sensors cannot fully capture. In applications involving slow-speed equipment—paper mill rolls, mining crushers, wind turbine main bearings—acoustic emission analysis often detects faults that would be invisible to conventional vibration measurement.
From Data to Decision
The translation from raw measurement to actionable recommendation is where field judgment becomes indispensable. A vibration report that lists fault frequencies without operational context is of limited use to a maintenance manager weighing a planned shutdown against continued production.
Experienced analysts understand this. Their reports are written not for other analysts but for operations leaders who need clear, defensible guidance. A well-structured finding might read: Bearing defect frequencies are present at 3.2 times running speed on the drive-end bearing of Motor 14-B. Amplitude trending indicates a fault progression rate consistent with failure within four to eight weeks under current load conditions. Recommended action: schedule replacement during the next planned outage or within thirty days if load increases.
That sentence represents the distillation of sensor data, historical trending, load history, and machine-specific knowledge into a single operational directive. It is the product of field expertise, not software.
"The software generates the spectrum," one analyst noted. "I generate the recommendation. Those are two completely different things."
The Business Case, Measured in Avoided Downtime
The economics of predictive maintenance through vibration analysis are well-documented. Industry estimates consistently place the cost of unplanned downtime in manufacturing environments between three and five times higher than the cost of planned maintenance. In continuous-process industries—refining, paper, chemicals, food processing—the ratio can climb higher still.
A formal vibration monitoring program, including field measurement rounds, data analysis, and reporting, typically runs between $50,000 and $250,000 annually for a mid-size industrial facility, depending on the number of assets monitored and the frequency of measurement. A single avoided catastrophic failure—particularly one involving secondary damage to connected equipment—can return that investment many times over.
Beyond the arithmetic, there is an operational confidence that comes from knowing the condition of critical assets. Maintenance managers who receive monthly vibration reports make better decisions about parts inventory, contractor scheduling, and production planning. That confidence has a value that does not appear cleanly on a spreadsheet but is felt across every department that depends on uptime.
Ground-Level Work in a Data-Driven World
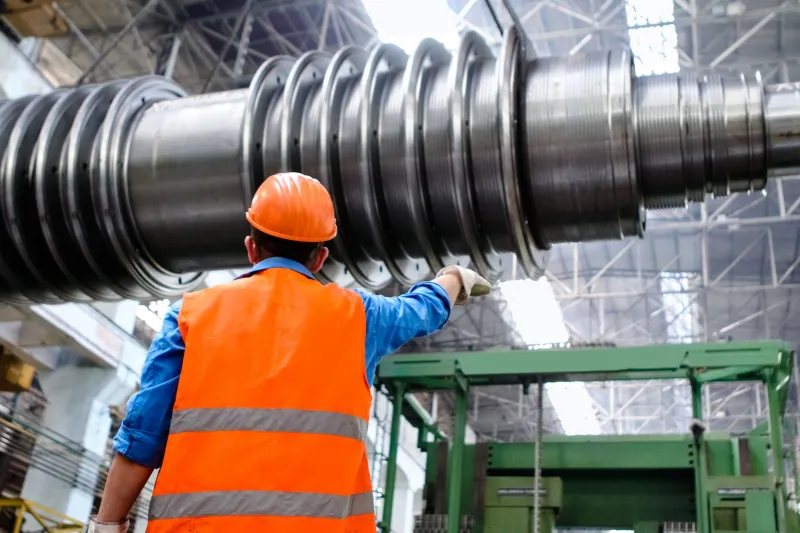
Vibration analysis is sometimes described as a purely technical discipline—a matter of sensors and software. The technicians who do it full-time would offer a more nuanced account. Getting accurate readings from a running machine requires physical access, mechanical knowledge, and situational awareness that no remote monitoring system fully replicates.
Probes must be placed consistently at designated measurement points to ensure trending integrity. Ambient conditions—temperature, nearby machinery, structural resonances—must be understood and accounted for. Anomalies that appear in the data must sometimes be walked back to the machine itself, with the analyst placing a hand on a bearing housing or listening through a stethoscope to correlate what the spectrum suggests with what the machine is actually doing.
It is, in the end, ground-level work. The kind where expertise is earned in plant aisles and equipment rooms, not conference rooms. The machinery speaks in a language of physics. These technicians are the ones who have learned to listen.